Yingzoom 3rd Generation Wheel Hub Bearing Assembly Line is a fully automated production and inspection system designed for high-efficiency assembly of third-generation wheel hub bearing units.
The complete line integrates automatic feeding, demagnetization, cleaning, drying, bolt press-fitting, oil slinger ring assembly, comprehensive inspection, grease filling, steel ball loading, seal ring press-fitting, angular clearance inspection, riveting, runout and torque testing, vibration and ABS testing, laser marking, anti-rust treatment and final alignment.
With a cycle time of ≤10 seconds per set, the system provides stable, continuous and traceable production for high-volume wheel hub bearing manufacturing.
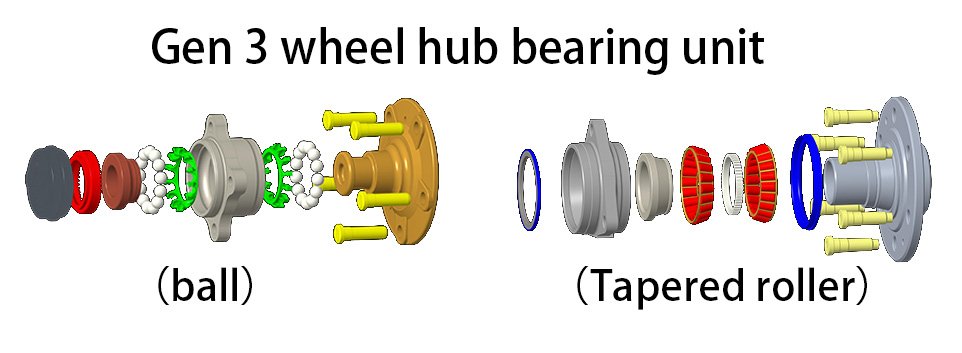
Working Product Size Range
| Nominal OR Outer Diameter: | Φ80~Φ180mm |
| OR Width: | 50~100mm |
| Nominal IR Bore diameter: | Φ20~Φ60mm |
| Inner Flange Width: | 50~150mm |
| Inner Flange Outer Diameter: | Φ100~Φ180mm |
| Note: The above specifications are subject to change according to customer requirements. | |
| Name | Automatic Gen 3 Hub Bearing Assembly Line(Ball,Taper Roller) |
| Cycle Time | ≤ 10S |
| Frame | 8080 Square Tube Surface Spray Coating |
| Measurement System | Keyence/TESA/MAPOSS/Oriental Measuring Instrument |
| Electric Control System | Siemens/Mitsubishi/Omron PLC 10 Inch Color Touch Screen |
| Safety Protective Cover | Aluminum Alloy Frame+Safety Grating |
| Loading And Unloading Mechanism | Automatic Loading And Unloading |
Main Technical Parameter
Key Features
High-Speed Production
Cycle Time: ≤10 s/set
The optimized production layout and synchronized servo-driven systems enable high-speed continuous operation while maintaining stable assembly quality.
Modular Fast Changeover
The production line adopts modular quick-change tooling, significantly reducing model changeover time.
Whole-line model changeover: approximately 3 hours / 3 operators
This design allows manufacturers to efficiently switch between different wheel hub bearing models while minimizing production downtime.
Fully Automatic Production
The entire production process is automatically connected from loading to unloading.
Loading Direction: Left → Right
Operators: 1–2 persons for the complete line
The automated material handling system ensures smooth and stable transfer of bearings between each process station.
Stable & Damage-Free Material Handling
Throughout the production process, bearings are transported and processed smoothly to minimize the risk of:
- Dents
- Scratches
- Collision damage
- Handling defects
From automatic loading through final unloading, the entire material flow is designed for stable, continuous and damage-controlled operation.
Intelligent Quality Control & Traceability
The third-generation wheel hub bearing assembly line integrates comprehensive inspection, data management and quality control functions throughout the production process.
Real-Time Process Monitoring
Critical production parameters can be monitored, recorded and evaluated, including:
- Pitch measurement
- Steel ball specification
- Calculated internal clearance
- Grease grade
- Grease injection quantity
- Press-fitting pressure
- Press-fitting displacement
- Press-fitting height
- Runout
- Angular clearance
- Negative clearance
- Assembly height
- Torque
- Vibration
- ABS testing results
Each inspection station provides visualized production data and statistical analysis.
SPC Data Management
Every inspection station is equipped with SPC statistical functions and production data storage.
Data Management Features
- Data retention for up to 6 months
- USB data export
- Production quantity statistics
- OK quantity statistics
- NG quantity statistics
- Measurement data recording
- Inspection result visualization
- NG reason identification
- Defect location identification
- Parameter modification time records
This enables manufacturers to establish a more complete production quality traceability system.
Intelligent NG Management
Each machine is equipped with a dedicated lockable NG bin and full-bin alarm.
The system provides a 1-to-1 correspondence between NG inspection data and the actual NG product, helping operators quickly identify and trace non-conforming products.
The equipment also includes standard reference part verification reminders, supporting consistent inspection accuracy during production.
Comprehensive Safety & Alarm System
The assembly line incorporates multiple levels of automatic monitoring and alarm functions.
The system can monitor and provide alarms for:
- Missing steel balls
- Missing components
- Abnormal press-fitting pressure/displacement
- Insufficient bolts
- Insufficient grease
- Low steel ball level
- Abnormal air pressure
- Servo motor overload
- Abnormal rotation speed
- Abnormal vibration/ABS testing conditions
- Equipment operation abnormalities
- NG product confirmation
- Safety door opening
This comprehensive alarm architecture helps operators identify abnormal conditions quickly and reduce production risks.
Advanced Inspection & Assembly Technology
The production line combines precision assembly, automated inspection and intelligent data management into one integrated manufacturing system.
Critical press-fitting stations continuously monitor pressure-displacement curves, allowing the system to identify abnormal press-fitting conditions during both intermediate and final positions.
The inspection system can automatically distinguish between OK and NG products, send non-conforming products to the corresponding NG lane, and record the inspection results for subsequent analysis and traceability.
Industrial Design & Safety Protection
The machine frame is manufactured using welded structural steel and aluminum alloy profiles, providing a rigid and stable platform for high-precision assembly.
Key design features include:
- Heavy-duty welded machine frame
- 80 × 80 mm structural square tubing
- Precision-machined 30 mm carbon steel base plate
- Aluminum alloy upper frame
- Transparent visual safety doors
- Protective acrylic covers
- Surface-treated structural and tooling components
- Hard chrome plating, black oxide or anodizing where required
- MC Nylon, POM and polyurethane materials for impact protection
The overall design combines industrial durability, precision and modern visual appearance.
Power & Utility Requirements
Electrical Power: AC 380 V, 50 Hz
Compressed Air: 0.4–0.6 MPa
Air Treatment: Oil mist filtration + automatic drainage system
PLC & Software Management
The PLC programs are fully commented to provide clear information for alarms and equipment status.
The control system provides clear visualization of:
- Equipment status
- Production information
- Inspection results
- OK / NG status
- Alarm information
- Process parameters
- Statistical data
Access to the PLC and HMI/PC programs is provided to the buyer after completion of the final payment, according to the agreed commercial terms.
Assembly Line Process Flow
A: Shaft Wheel
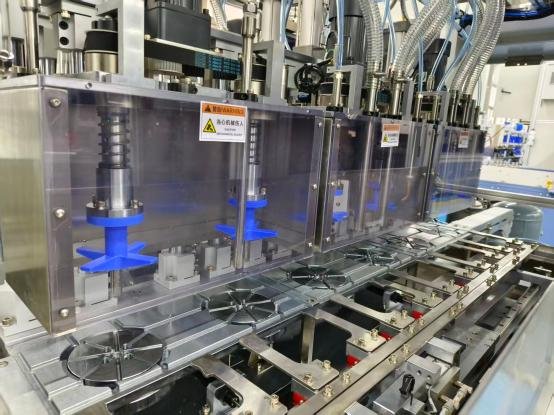
1.Shaft Wheel Demagnetization & Cleaning Machine:
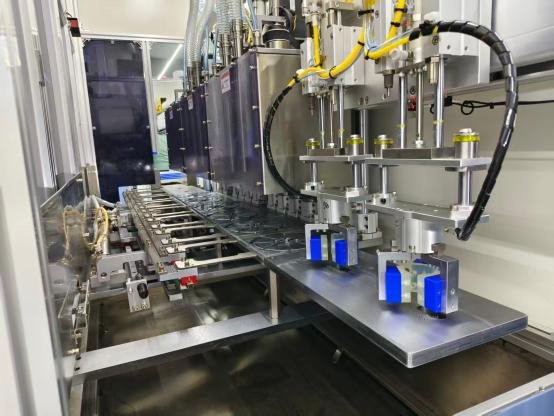
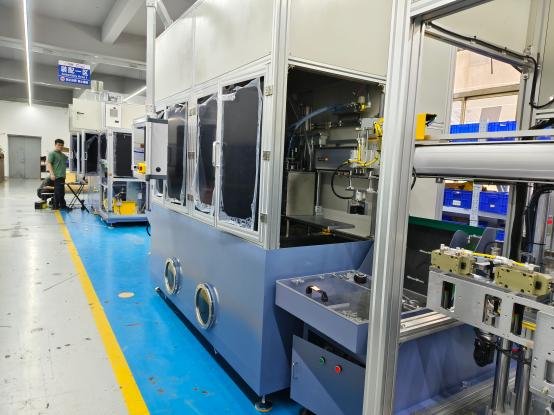
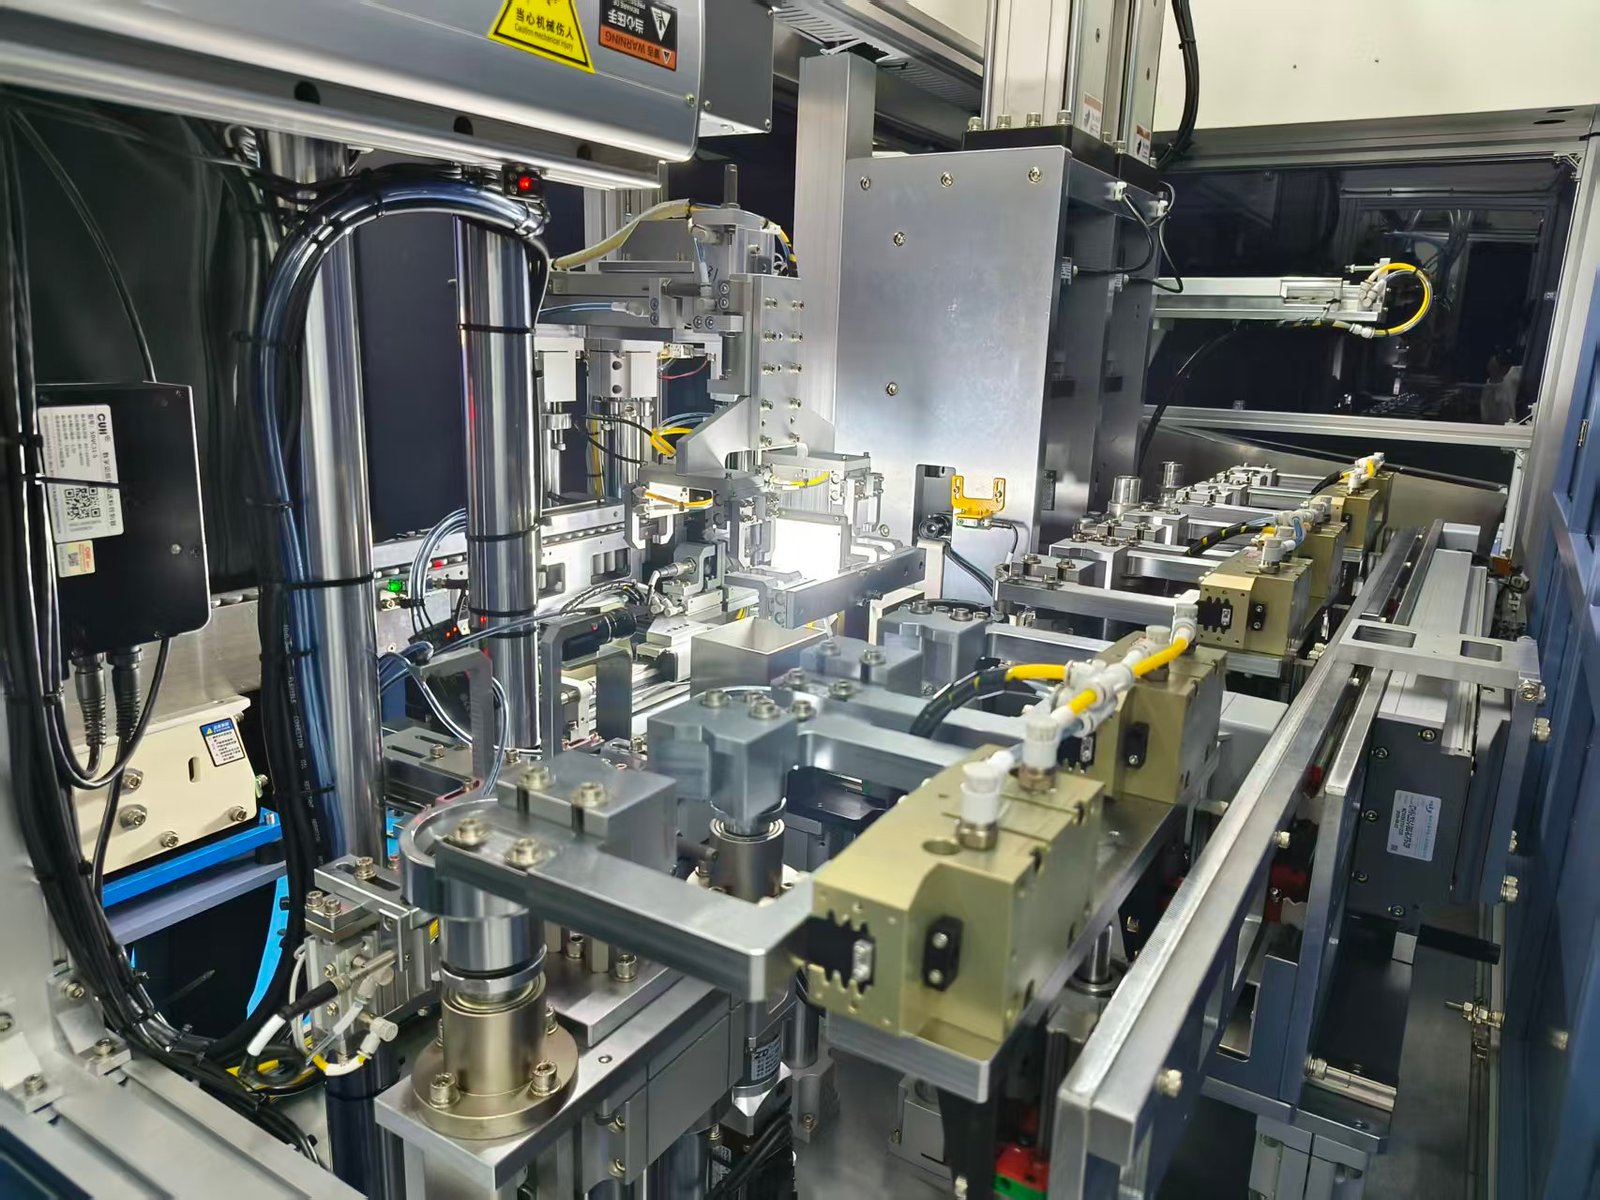
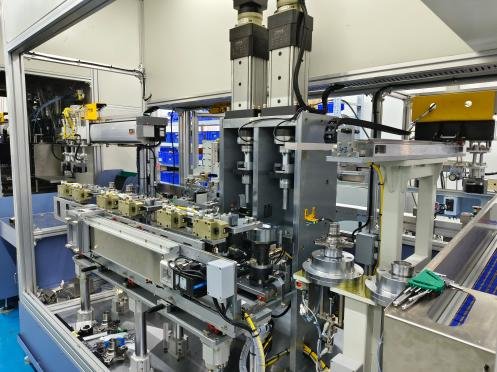
- Automatic Dual-Station Bolt Press-Fitting Machine:
- Automatic Shaft Wheel Oil Slinger Ring Press-Fitting & Detection Machine:
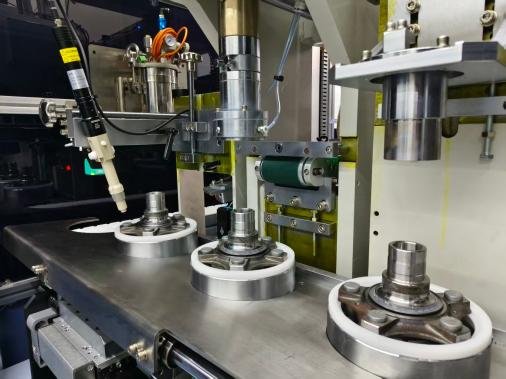
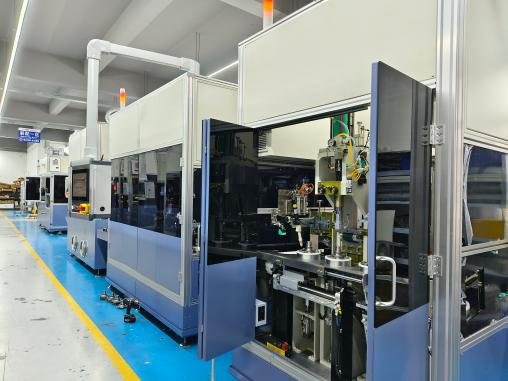
(Shaft Wheel Demagnetization & Cleaning Machine:Stainless Steel Conveyor Belt Feeding → Servo Linear Module Controls The Robotic Arm For Gripping and Feeding → Demagnetization → Rotary Cleaning → Spin Dry → Blow Dry) → (Dual-Station Bolt Press-Fitting Machine:Bolt Feeding → Vision Inspection: Bolt Length, Thread Pitch → Dual-Station Bolt Press-Fitting → Position Tolerance Detection → Discharge) → (Apply Anaerobic Adhesive & Oil Slinger Ring Press Fitting:Apply Anaerobic Adhesive → Oil Slinger Ring Press Fitting → Press-fit In Place Detection)
B: Outer Ring & Inner Ring
Outer Ring & Inner Ring Two-channel Demagnetization, Cleaning Machine:
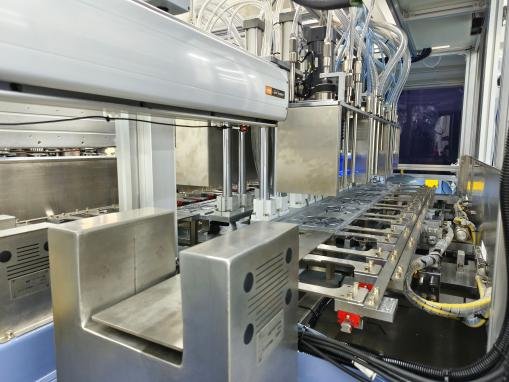
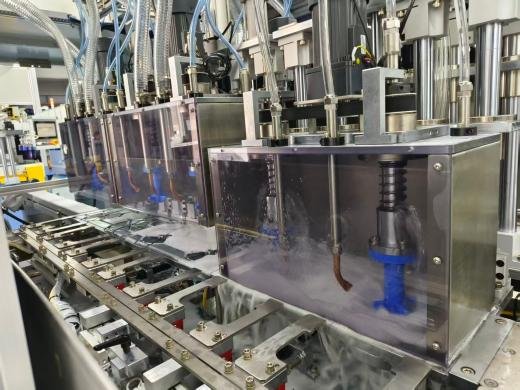
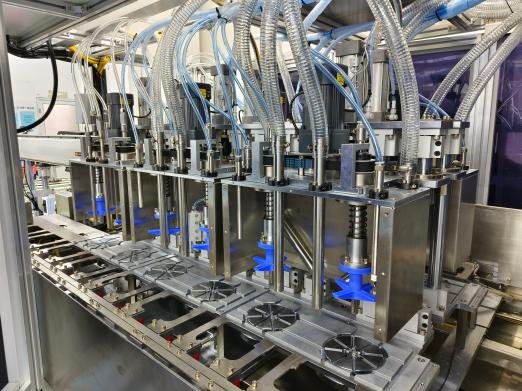
Stainless Steel Conveyor Belt Feeding → Servo Linear Module Controls The Robotic Arm For Gripping and Feeding → Demagnetization → Rotary Cleaning → Spin Dry → Blow Dry
C:Automatic Three-Channel Comprehensive Inspection Machine
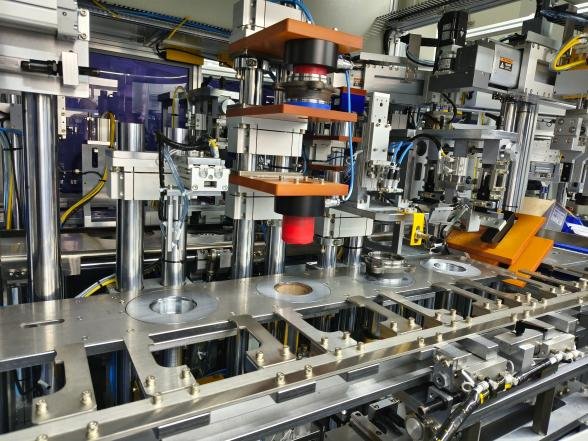
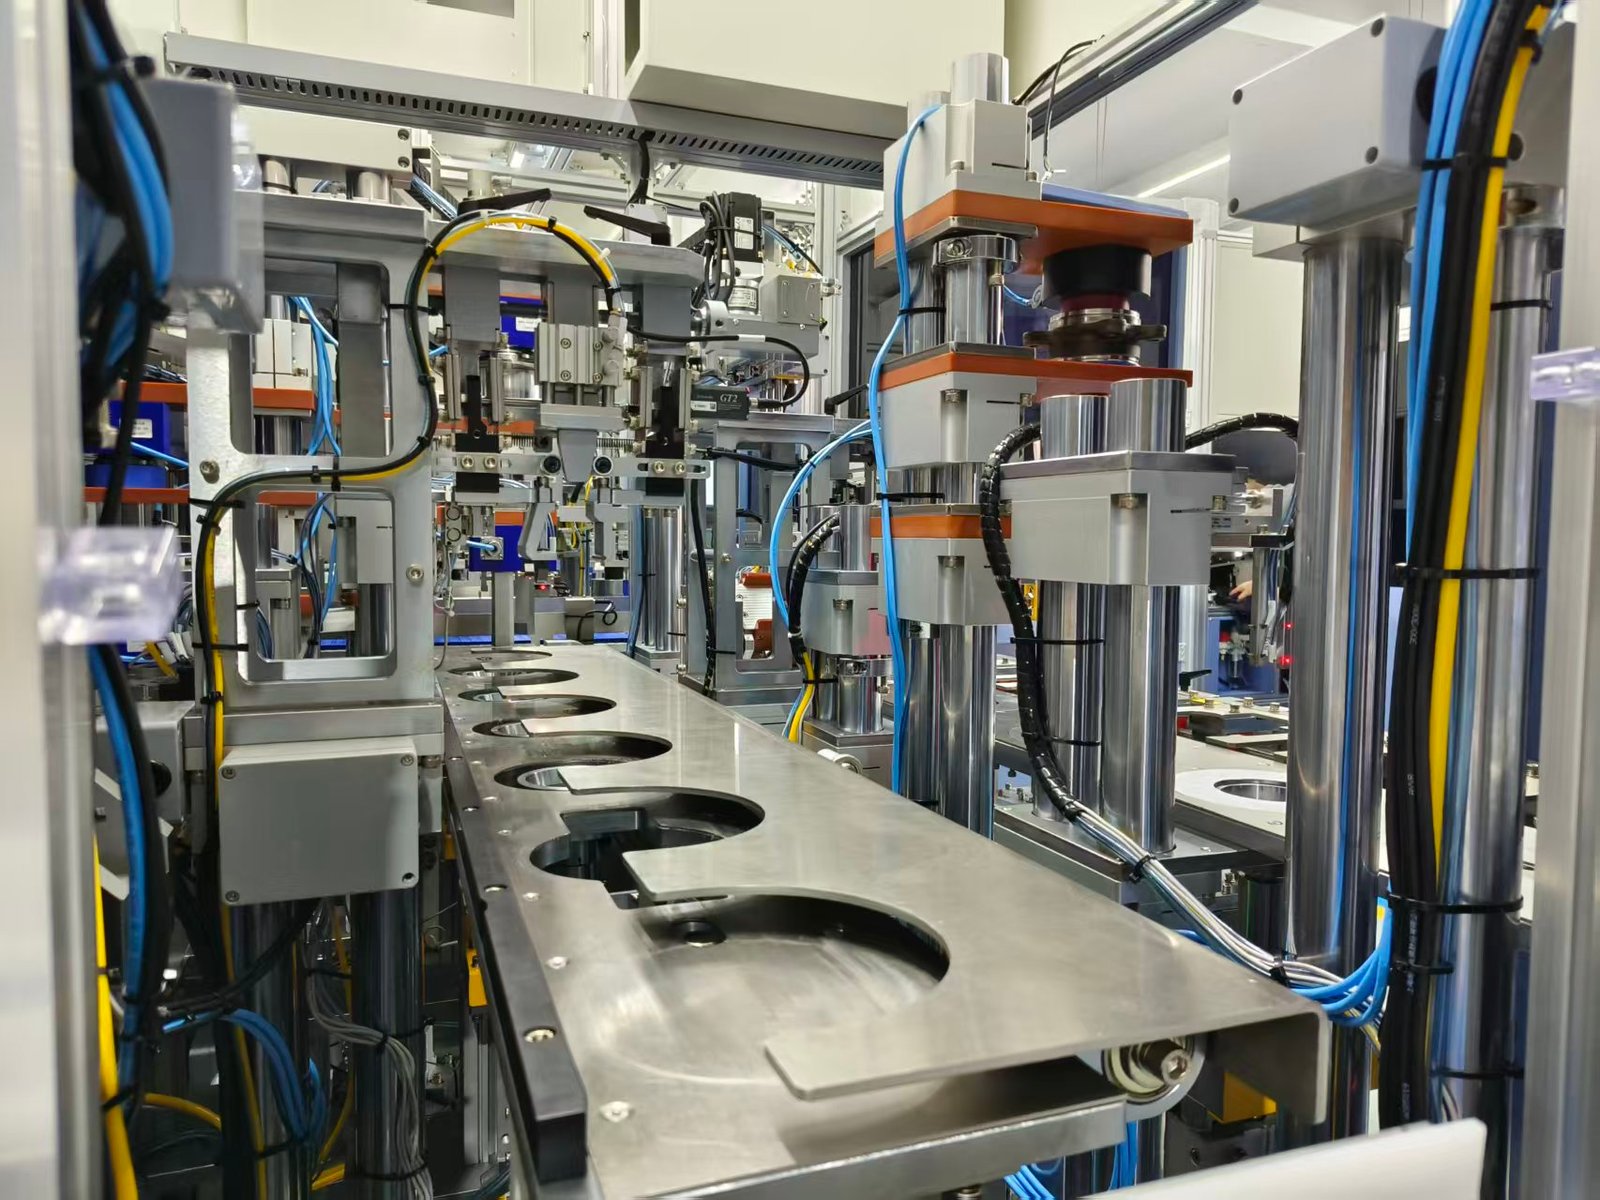
- Outer Ring Channel:Outer Ring Fit Outer Diameter Detection → No Super Finish Detection → Hardness Detection → Raceway Crack Detection
- Inner Ring Channel:Inner Ring Inner Diameter Detection → No Super Finish Detection → Hardness Detection → Raceway Crack Detection
- Shaft Wheel Channel:Press-fit Shaft Diameter Detection → Wheel Fit Outer Diameter Detection → No Super Finish Detection → Hardness Detection → Raceway Crack Detection
D:Automatic Three-Channel Sorting & Turntable Storage Library
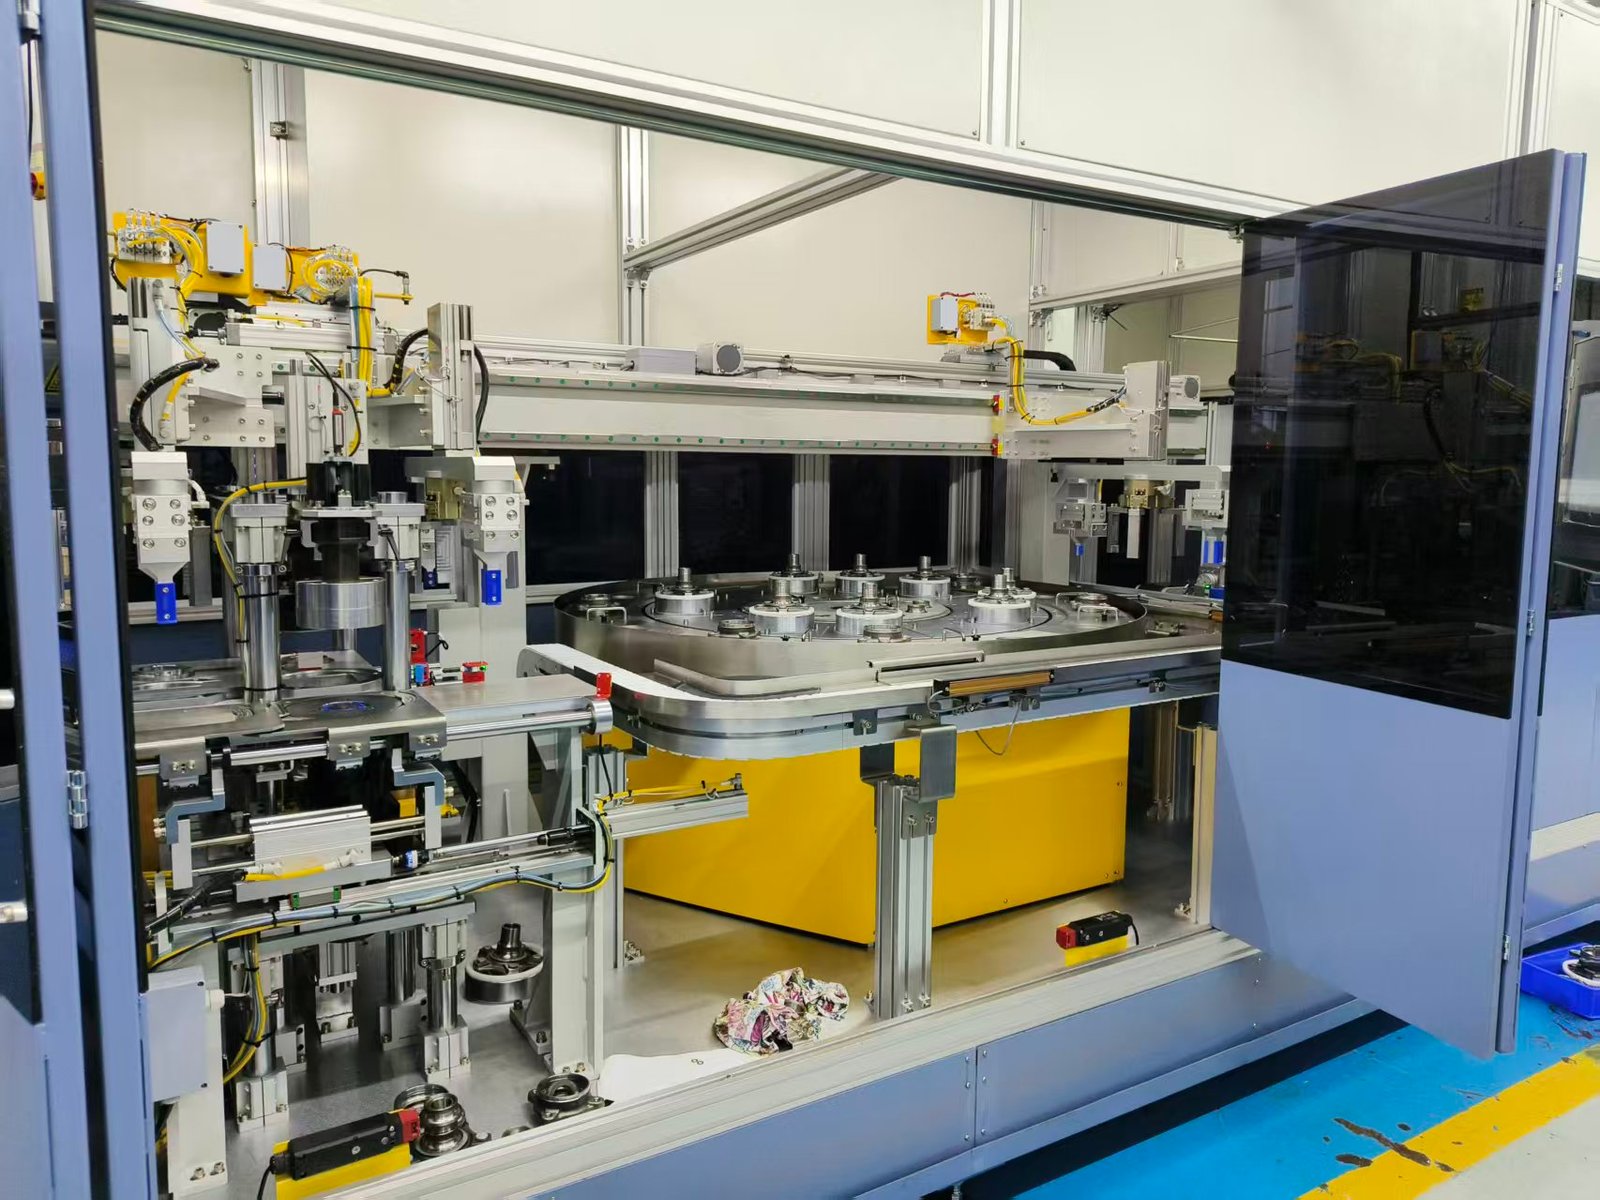
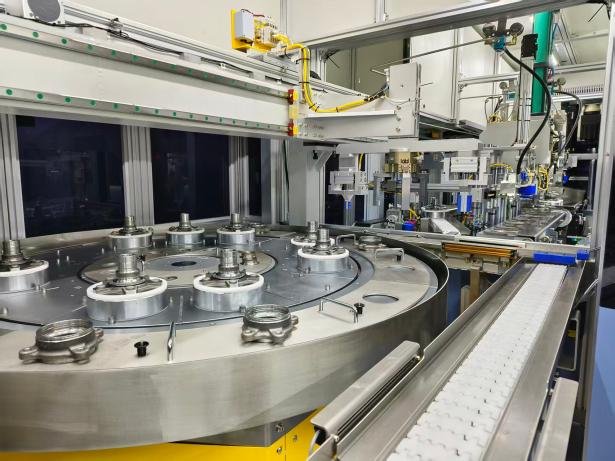
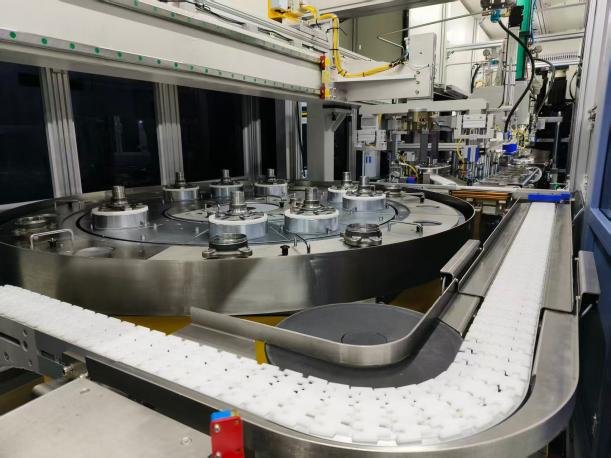
Outer Ring/Shaft Wheel/ Inner Ring Pitch Detection → Deposit into Turntable Storage Library → Discharge
E:Automatic Outer Ring Grease Injection & Weighing & Ball Adding And Assembling & Seal Ring Press Machine
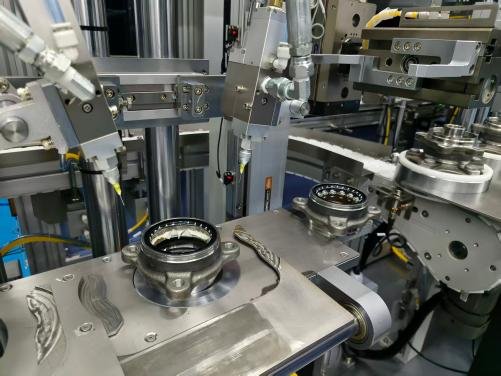
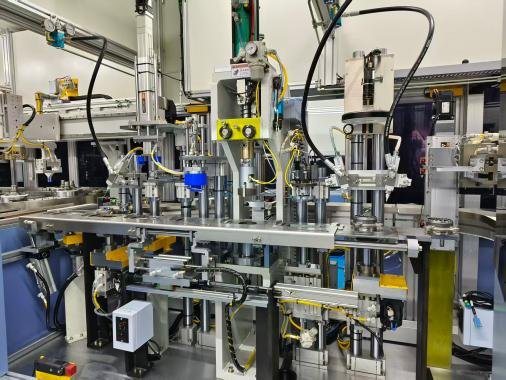
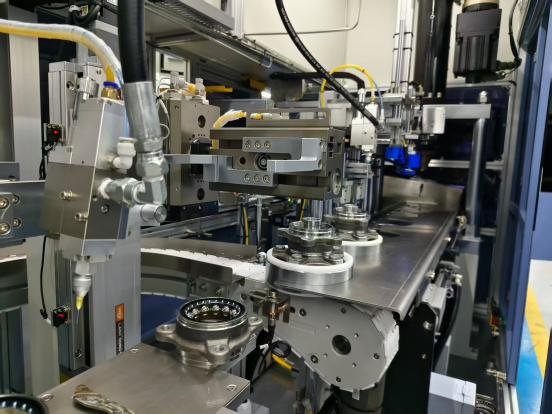
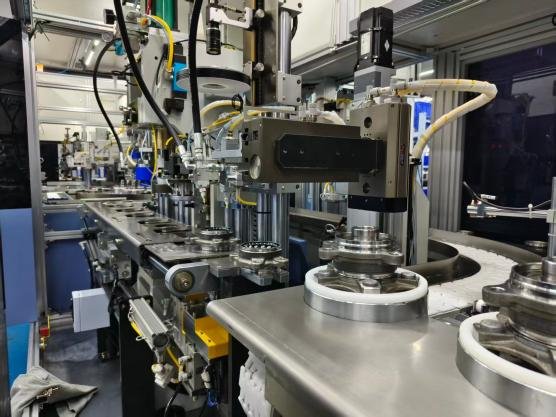
(Outer Ring Weighing → Grease Injection → Check Grease Injection Quantity By Weighing → Ball and Cage Assembly Pressed Into → Seal Ring Press Fitting → Press-fit In Place Detection → Grease Injection On Lip → Vision Inspection:No Grease Injection/Missing Steel Ball and Cage Assembly → 180° Flip Assembly (Oil slinger ring omission check and error-proofing inspection prior to assembly)→ Weighing → Grease Injection (Needle-type Grease Injection) → Check Grease Injection Quantity By Weighing → Put In Steel Ball and Cage Assembly → Place Inner Ring → Press Inner Ring
F:Automatic Ball and Cage Assembly Sorting Feeding Machine
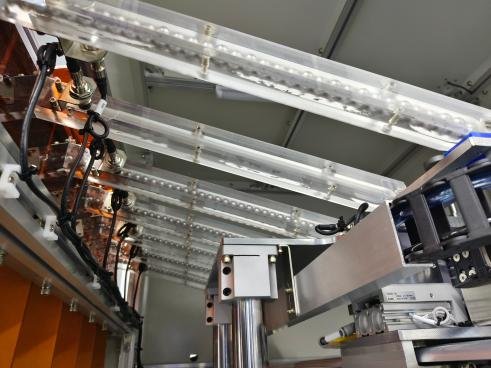
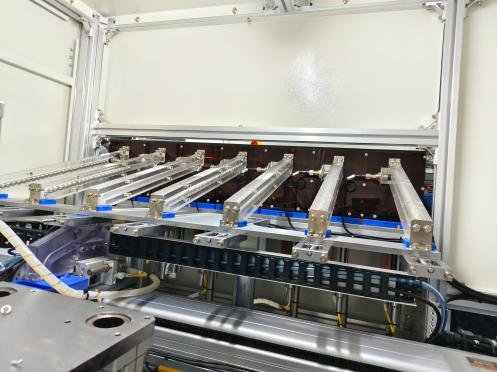
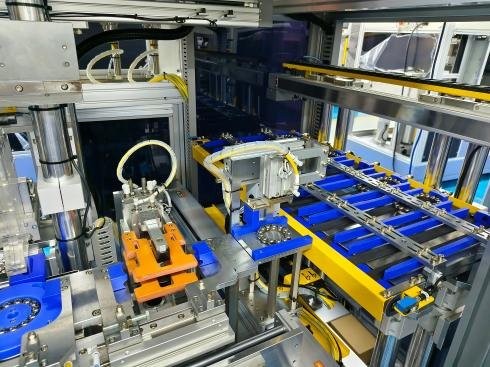
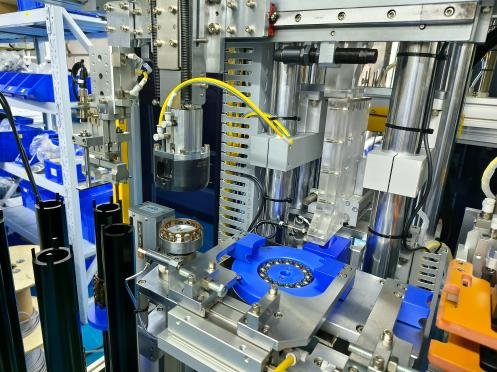
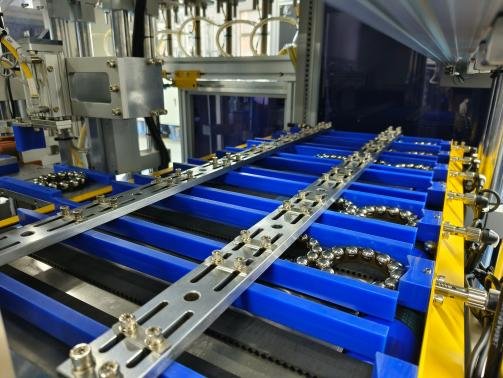
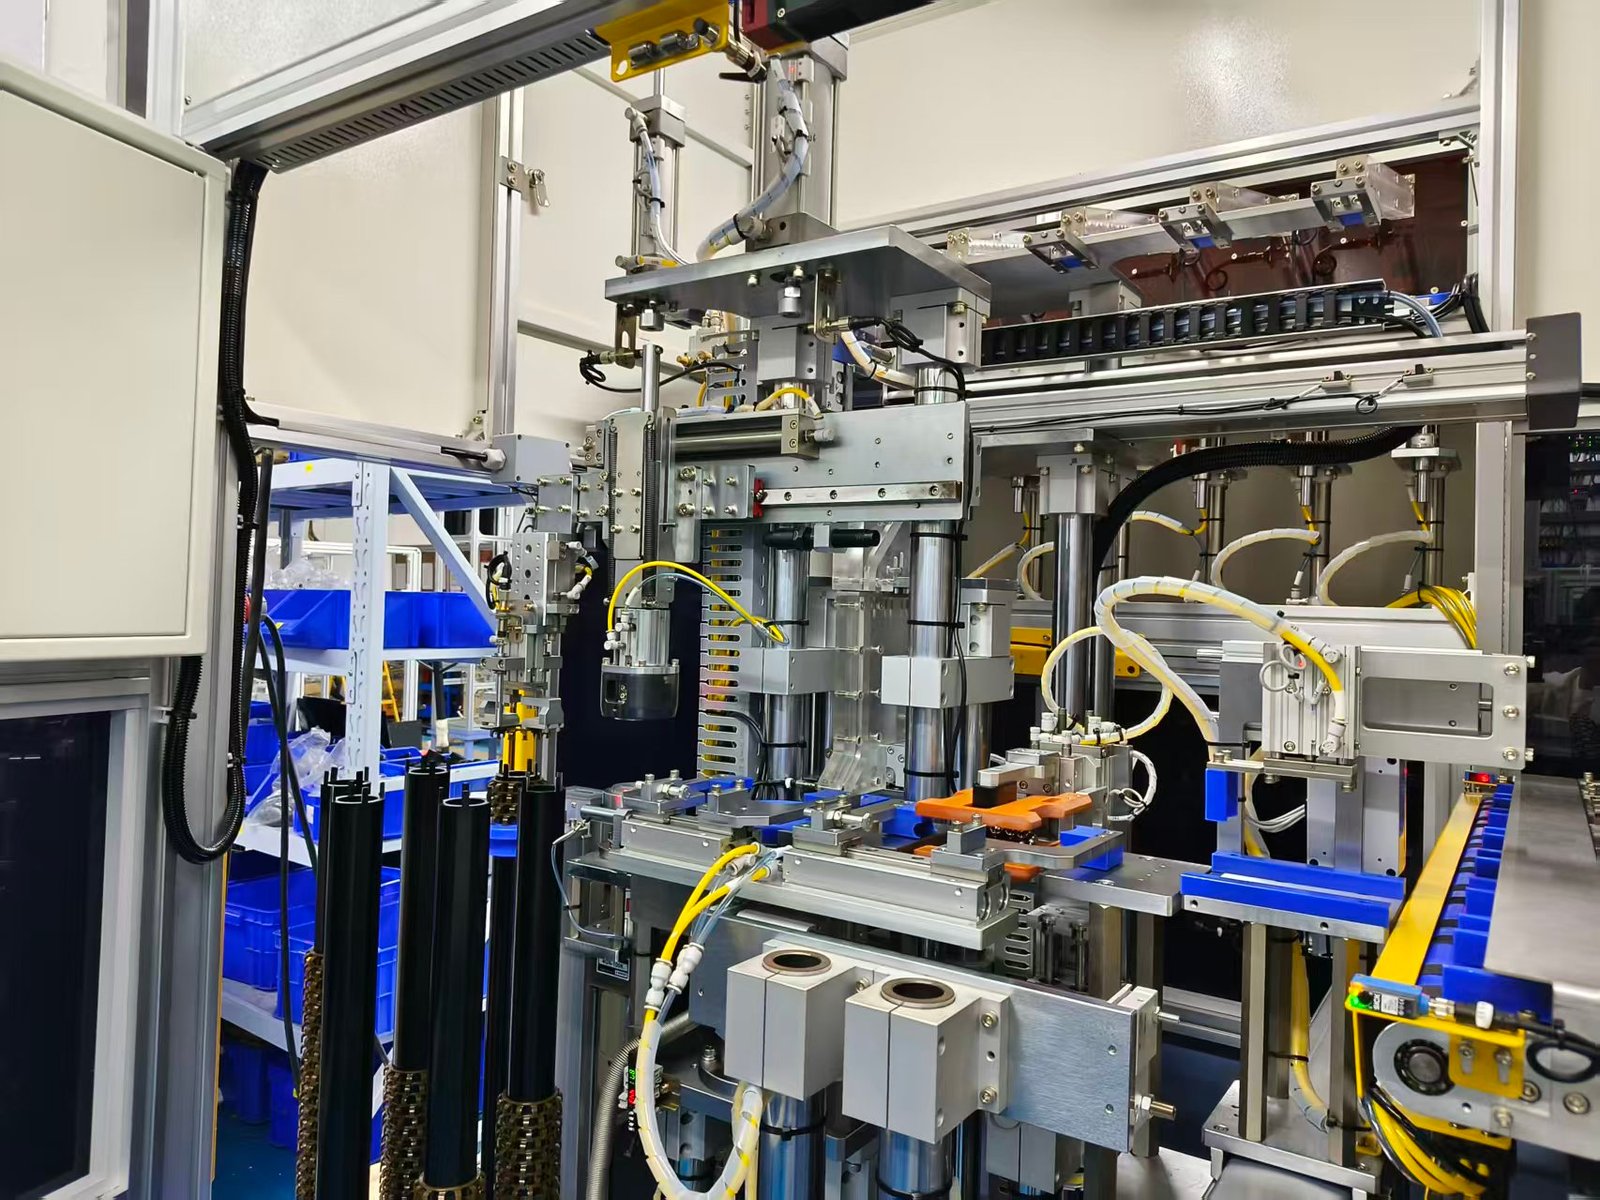
Cage Feeding → Cage Find Location → Put In Steel Ball → 180° Flip → Classifying Stock Library(7 Storage Silos) → Discharge
G:Automatic Angular Clearance Detection & GSY Press-Fitting Detection Machine:
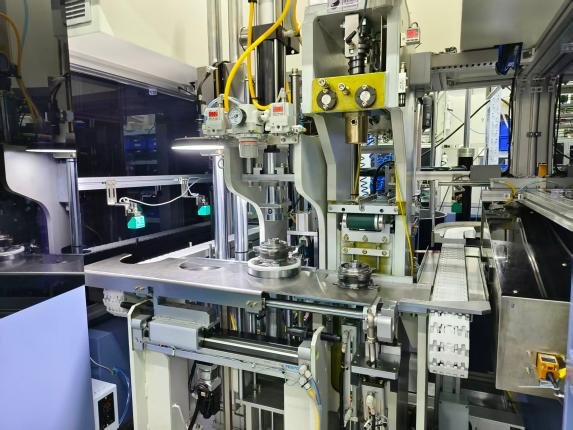
Automatic Pallet Feeding → Find Location → Angular Clearance Detection → GSY Press Fitting → Discharge
H:Automatic End Spline/Hemming Rotary Rolling (Pre-pressed Rotary Riveting)
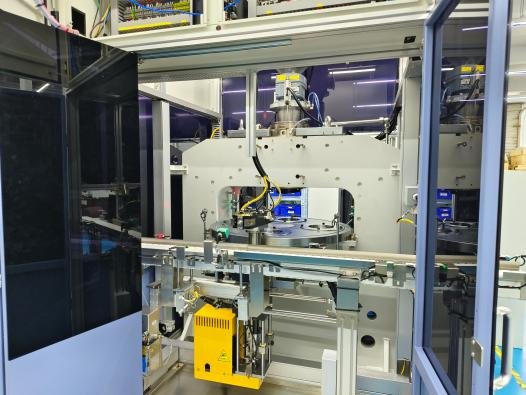
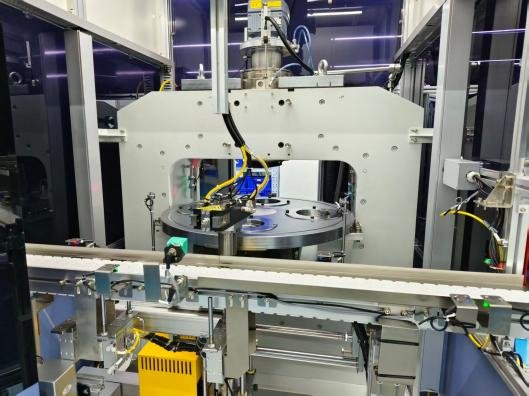
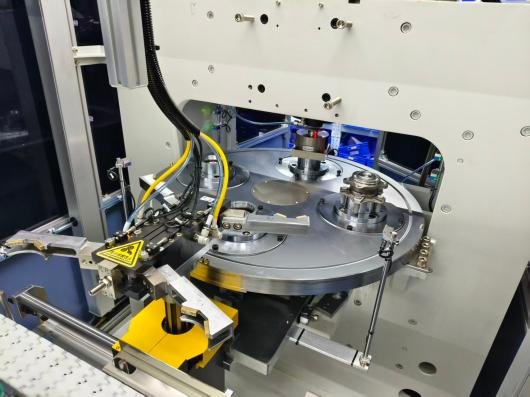
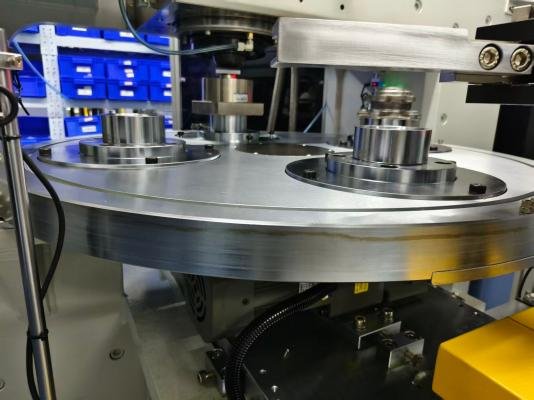
Pallet Conveying:Oil Application → Riveting Hemming → Discharge
I:Automatic Angular Clearance Detection & Hemming Crack Detection & Negative Clearance Detection & Assembly High Detection & GSY Secondary Press-Fitting Detection Machine
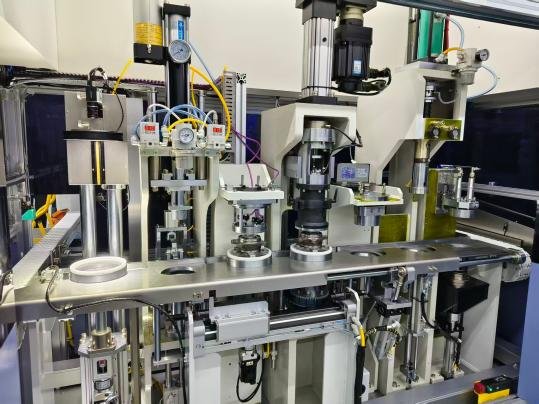
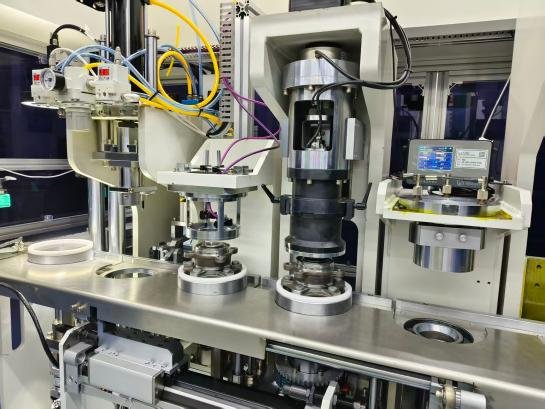
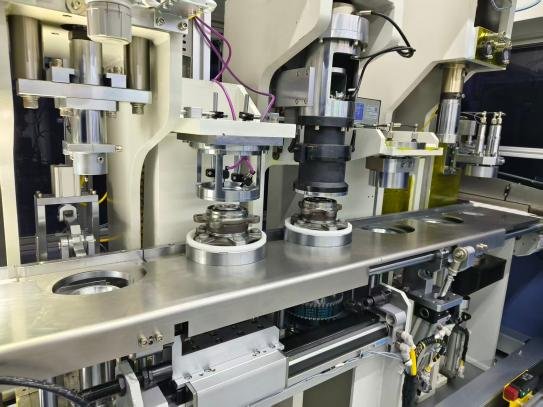
Hemming Crack Detection → Find Location → Angular Clearance Detection → Negative Clearance Detection(Rigidity Detection) → Assembly High Detection → GSY Secondary Press Fitting → Press-fit In Place Detection
J:Automatic End Spline Runout Detection & Torque Testing & End Cap Press-Fitting Detection Machine
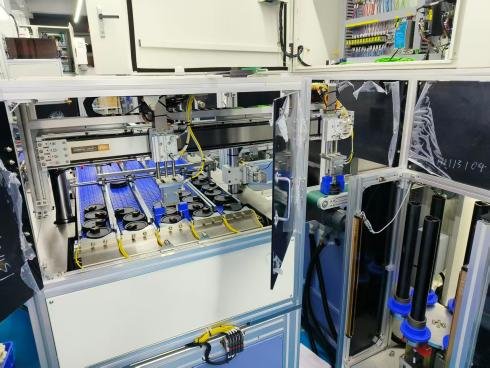
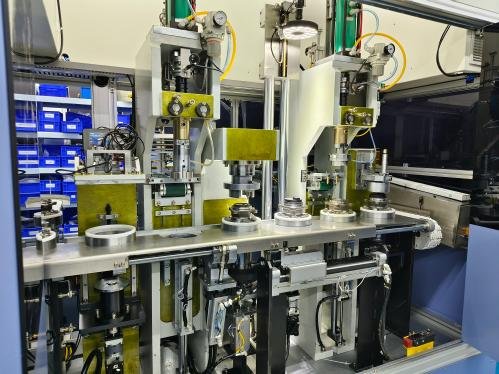
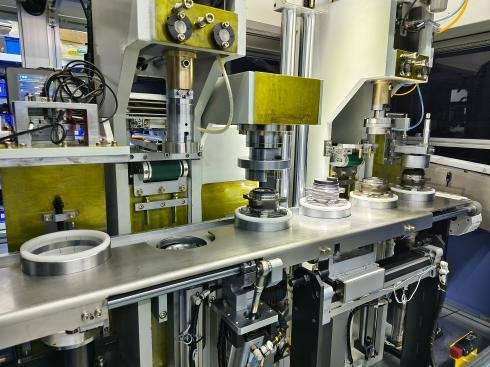
Find Location → Spline Runout Detection → Spline Protection Cover Press Fitting → Press-fit In Place Detection → Find Location → End Cap Press Fitting → Torque Detection
K:Finished Lathe (To be provided by the buyer)
L:Automatic End Face And Radial Runout Detection & Vibration Sound Detection & ABS Testing & Laser Marking Machine
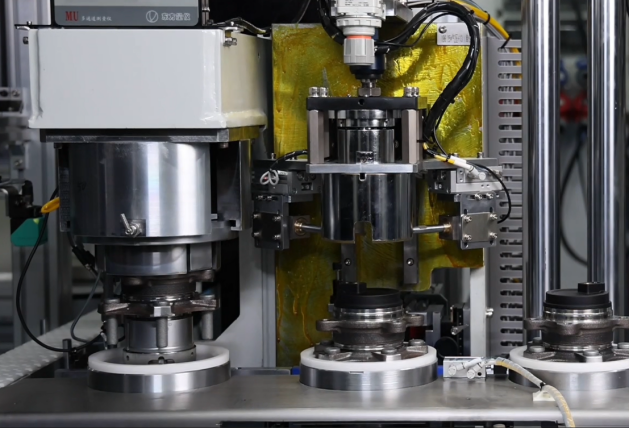
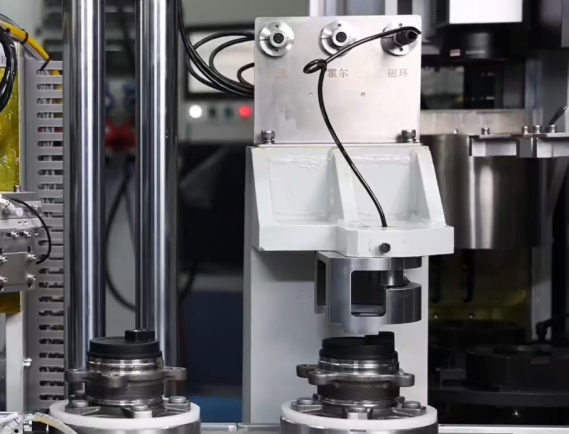
End Face And Radial Runout Detection → Find Location → ABS Detection → Vibration Detection → Find Location → Laser Marking And Scan QR Code → Discharge
M: Atomization Anti-rust & Standard Alignment Table
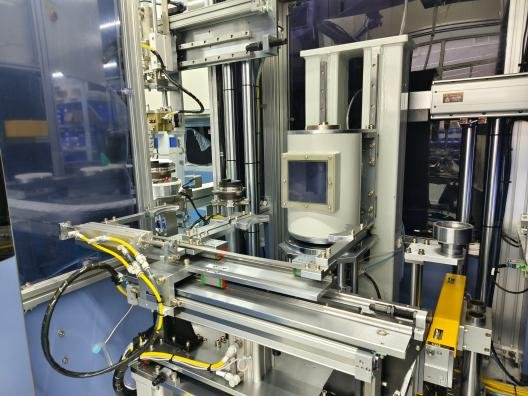
Atomizing Anti-rust → Automatic Alignment
Why Choose yingzoom?
01 — High Production Efficiency
≤10 seconds/set cycle time for high-volume production.
02 — Flexible Model Changeover
Modular quick-change tooling enables approximately 3-hour whole-line model changeover with 3 operators.
03 — Minimal Labor Requirement
Only 1–2 operators are required for normal operation of the complete line.
04 — Integrated Quality Control
Assembly, inspection, sorting and data management are integrated into one automated system.
05 — Complete Traceability
SPC, inspection records, production statistics and NG information provide comprehensive production traceability.
06 — Damage-Controlled Handling
Smooth automated material transfer minimizes scratches, dents and collision-related defects.
Reviews
There are no reviews yet.